Our Solutions

Medical & Pharmaceutical

Air & Vacuum Technology in Singapore’s Pharmaceutical Industry

Enabling Precision, Purity, and Innovation

  • Singapore has earned its reputation as Asia’s biomedical hub, driven by innovation, robust infrastructure, and world-class regulatory standards. At the heart of this success lies a range of enabling technologies—chief among them, air and vacuum systems. These systems are fundamental to sterile production, environmental control, material handling, and packaging in pharmaceutical manufacturing.
  • In environments where the slightest contamination can compromise a life-saving therapy, air and vacuum technologies ensure purity, precision, and compliance—forming the invisible backbone of Singapore’s pharmaceutical supply chain.

Key Applications Include:

Aseptic Filling and Sterile Drug Production

Vacuum technology enables clean, controlled transport and filling of drug solutions into vials, ampoules, and prefilled syringes—especially in aseptic fill-finish environments. These systems allow pressure differentials to be finely controlled, ensuring that no ambient contaminants enter the sterile zone. In high-speed filling lines, vacuum assists in container stoppering, capping, and leak testing—key to ensuring every unit meets global pharmaceutical safety standards.
Vacuum Drying, Lyophilization & Powder Processing

In pharmaceutical production, delicate compounds often degrade under heat. Vacuum drying and lyophilization (freeze-drying) are used to remove moisture under low pressure, preserving the biological activity of sensitive APIs, peptides, and biologics. This is crucial in producing powders, tablets, or injectable medications that require long-term stability.

Processes supported:

  • Freeze-drying of vaccines, plasma products, and biologics.
  • Drying of APIs or granules post-crystallization or solvent washing.
  • Solvent recovery using vacuum-assisted rotary evaporators or thin-film evaporators.
  • In Singapore’s biotech manufacturing plants, these systems enable efficient large-batch drying while minimizing risk of cross-contamination or thermal degradation.

Cleanroom Vacuum Packaging and Barrier Isolation

Pharmaceutical products are handled in cleanroom environments classified from ISO Class 5 to 8. Within these controlled zones, vacuum sealing and barrier packaging are critical. Products are often double-bagged in vacuum-sealed pouches to prevent particulate ingress and microbial contamination when transferred between cleanroom areas.

Dust Containment, Fume Extraction & Occupational Safety

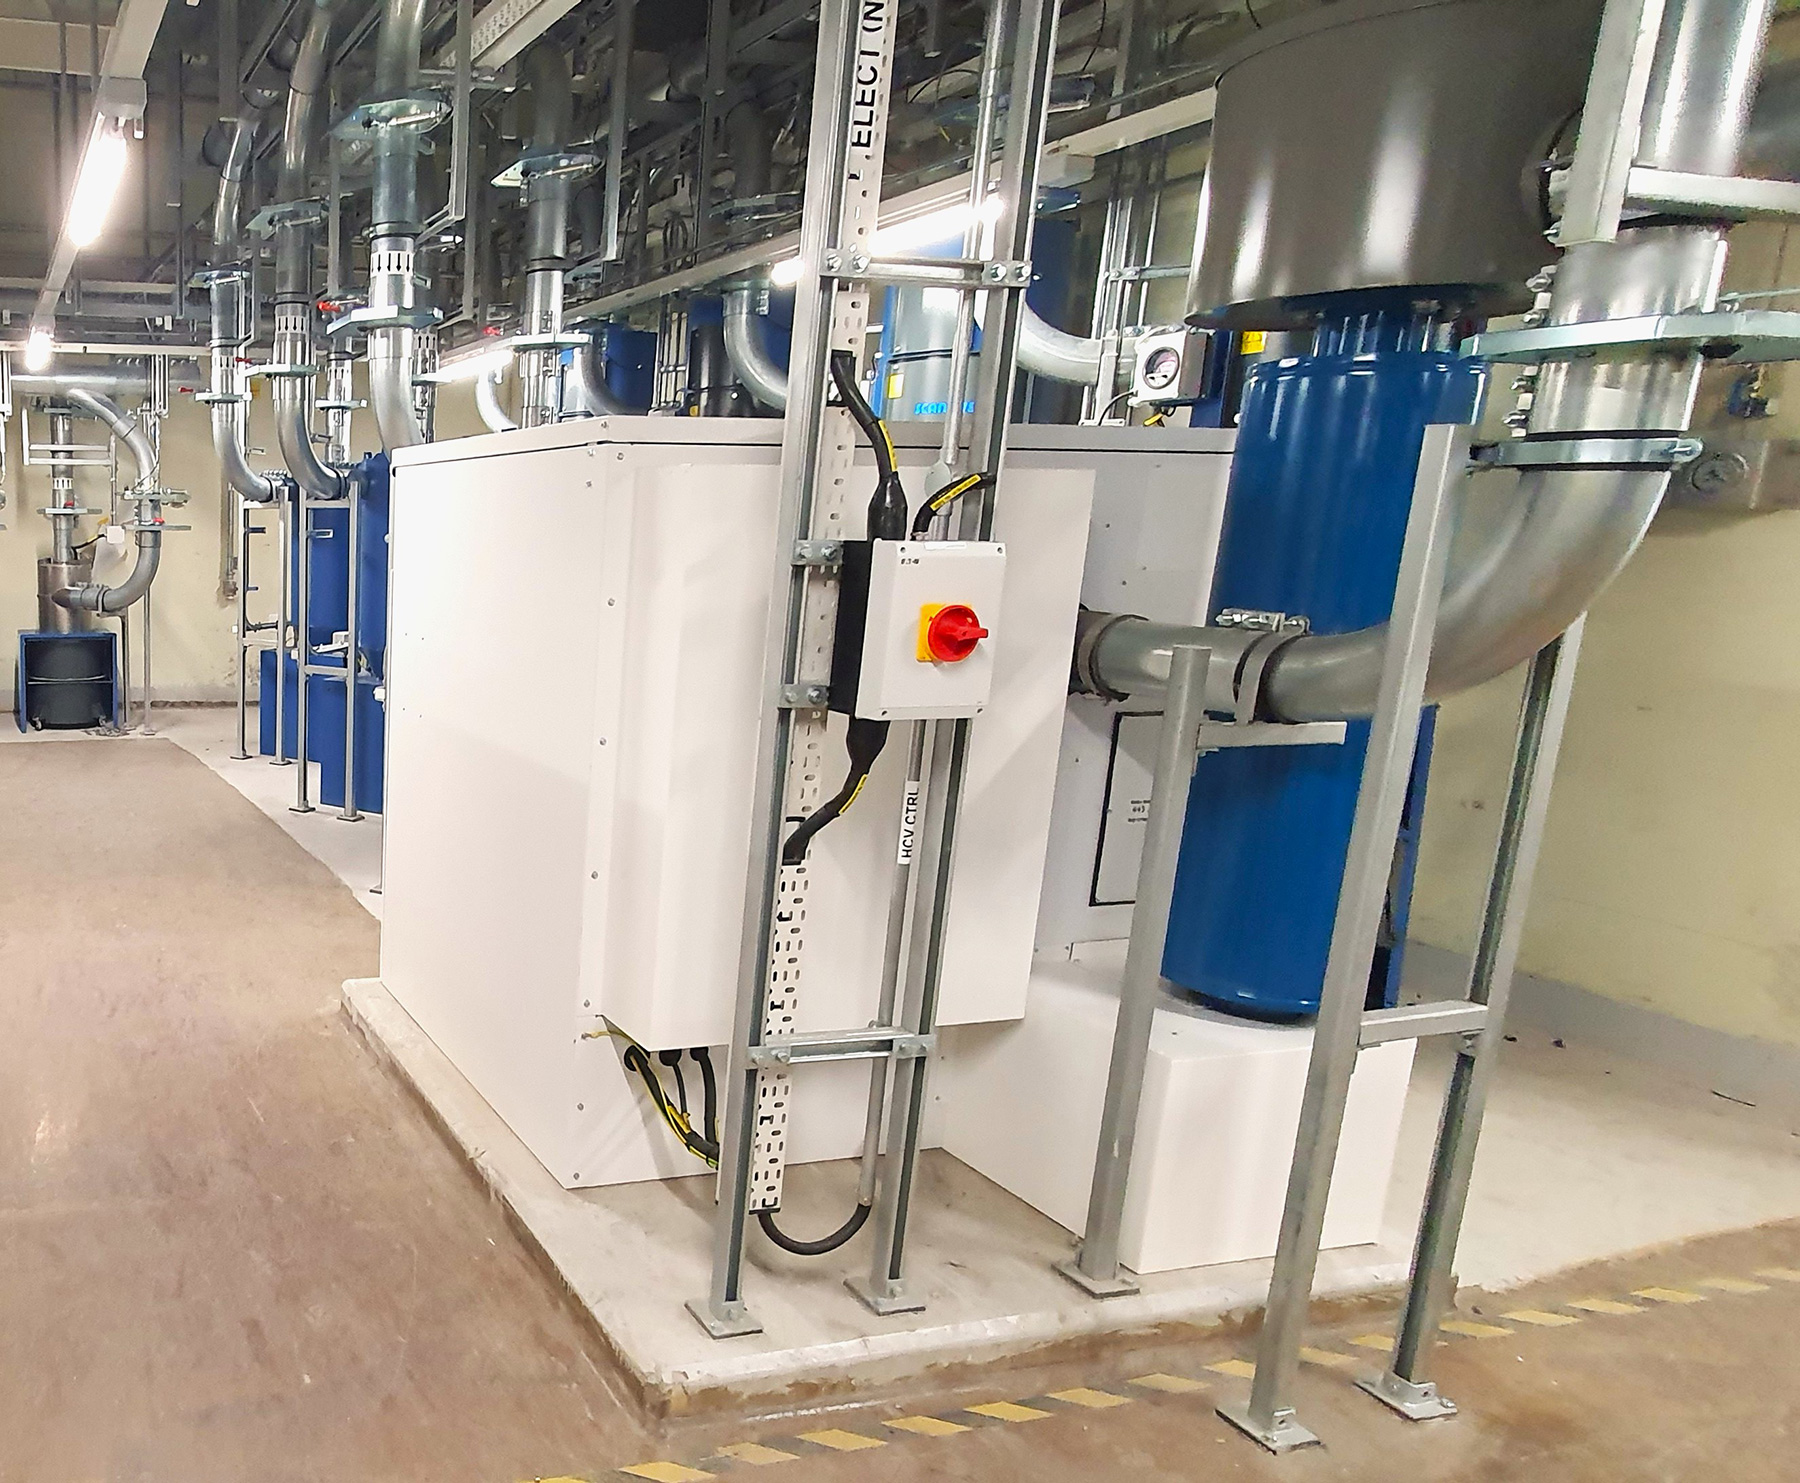
  • During powder processing—such as granulation, tablet pressing, or coating—vacuum systems are deployed for dust extraction and localized containment. These vacuum filtration systems protect both the operator and the product while ensuring regulatory compliance with HSA, NEA, and international standards like OSHA and GMP.
  • Typical units include:
  • High-efficiency particulate air (HEPA) filtered vacuum collectors
  • Centralized vacuum exhaust for coating pans and granulators
  • Negative pressure isolators for high-potency drug containment
  • This protects not only product quality but also personnel working with potent compounds such as oncology APIs.

Component Testing & Vacuum Leak Detection

  • In medical device manufacturing—ranging from catheters and tubing to implantables—vacuum-based leak testing and pressure decay tests are used to verify product integrity. Vacuum chambers are used for simulating sub-atmospheric conditions in transport scenarios or testing bubble-point leakage in packaging.
  • These test systems are critical in ensuring that devices are both functionally robust and safe for clinical use.

Singapore’s Competitive Edge in Vacuum-Driven Pharma Manufacturing

With strong government backing under the Biomedical Sciences Initiative and a robust regulatory environment, Singapore remains an ideal location for high-precision, vacuum-dependent pharmaceutical operations. The Health Sciences Authority (HSA) encourages advanced manufacturing with cleanroom integration, vacuum-controlled environments, and digital monitoring systems.

Vacuum technology supports:

  • Operational continuity with central vacuum utility systems
  • Modular manufacturing designs that integrate skid-mounted vacuum units
  • Environmental responsibility through solvent recovery and reduced energy consumption

Why It Matters

  • Patient Safety: Vacuum and air systems help eliminate contaminants from sensitive drugs.
  • Regulatory Compliance: These systems help facilities meet HSA, GMP, and FDA requirements.
  • Energy Efficiency: Advanced air/vacuum setups reduce energy consumption and support sustainability goals.
  • Scalable Production: Modular vacuum and compressed air systems scale easily with batch or continuous production models.

Conclusion

  • As Singapore continues to lead in pharmaceutical innovation, air and vacuum technologies remain critical to this progress. From supporting cutting-edge biologics to ensuring sterile, scalable drug production, these systems serve as essential enablers of efficiency, compliance, and patient safety.
  • The invisible infrastructure of air and vacuum—quietly operating behind every cleanroom, vial, and batch—ensures that Singapore’s pharmaceutical industry remains trusted, world-class, and future-ready.

Success Stories and case studies:

Vacuum Drum Drying vs. Spray Drying for ABT-199

  • Comparative research on drying ABT-199 nanocrystals shows vacuum drum drying (VDD) offers superior redispersibility, tablet compressibility, and higher yields than spray drying. The findings highlight VDD as a leaner, more efficient alternative for solid oral dosage forms.
  • Reference Link: ( https://www.pharmaexcipients.com/news/vacuum-drum-drying/?)

Vacuum Tray Dryers Drive Efficiency Gains

Applications:

Technology

Brands:

Vacuum Inlet Filters, Traps, Silencers